How to Program a Multi Axis CNC Spinning Lathe for Beginners

Time:2026-11-01 Author:Henry
0%

Learning how to program a multi axis cnc spinning lathe for beginners starts with understanding how the machine shapes metal. A rotating blank meets a forming tool, and each programmed movement affects the finished profile. The control coordinates several axes, often including the spindle, tool slide, and tailstock. Small errors can leave visible ridges, uneven walls, or an incorrect rim. Start with the drawing, material, tooling, and machine limits—not with copied code. Measure the blank. Check the tool path. Keep hands clear of moving parts.

This guide explains the programming process in practical steps, from reading a profile to setting axis positions, feed rates, and safe clearances. It also covers simulation and cautious trial runs, because a screen preview cannot reveal every setup problem. A useful shop-floor reminder is: “Verify the motion before the metal moves.” That is an original teaching line, not a verified quotation. No source article or expert reference was provided, so I can’t responsibly attach it to a named CNC spinning specialist. Add a sourced expert name and exact quotation before publication. That matters. Reliable programming depends on clear machine documentation, measured setup details, and careful checks at the control. Expect to revise a first tool path; real parts can expose assumptions that looked fine on screen.
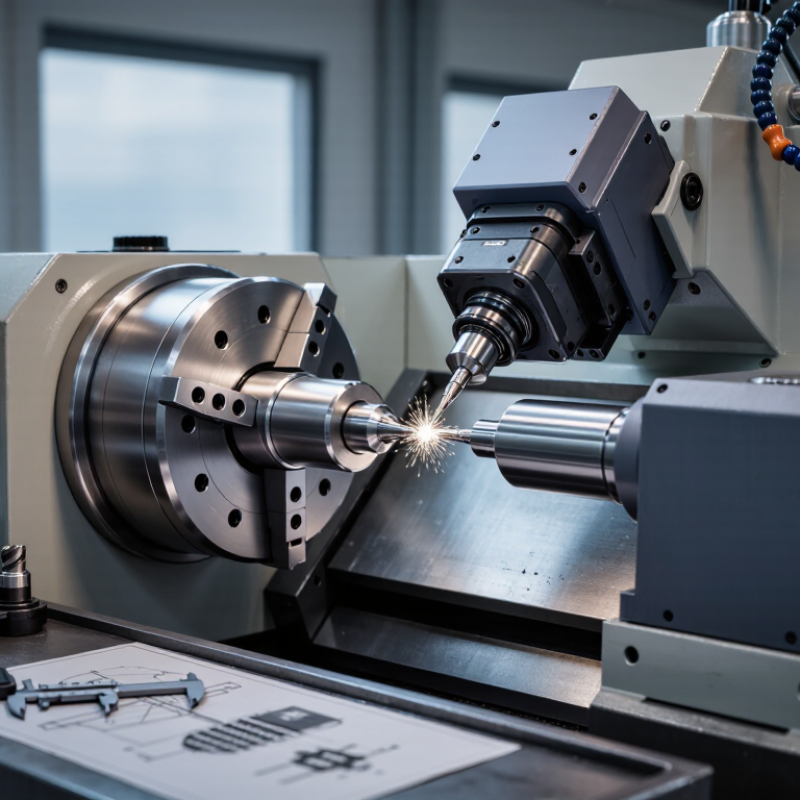
How to Program a Multi Axis CNC Spinning Lathe for Beginners

Understand the Multi-Axis CNC Spinning Lathe and Its Main Components

A multi-axis CNC spinning lathe shapes a rotating metal blank by pressing a roller against it over a mandrel. The spindle and chuck hold and turn the blank; the mandrel supports its inner profile. The forming roller applies pressure in controlled passes. These parts work together, so a small alignment error can leave uneven walls or surface marks.

The machine’s axes describe different movements. X usually moves the roller across the workpiece, while Z moves it along its length. The spindle’s C axis controls angular position, and some machines add another axis for more complex paths. Axis names and directions can vary by machine, so check its manual before writing a program. Small details matter. A tailstock may support long setups, while guards and sensors help monitor operation.

The CNC controller turns programmed coordinates and feed rates into machine motion. Beginners should identify each axis, the tool’s starting position, and the workpiece’s clamping method before planning a path. I would also verify clearance with a cautious dry run; it is easy to overlook how a roller approaches a shoulder. Not every setup behaves as expected. Material thickness, mandrel shape, and roller geometry all affect the forming result, so trial measurements are useful before adjusting a program.

Identify the Axes, Machine Coordinates, and Control Functions

A multi-axis spinning lathe becomes easier to program when each movement has a clear reference. ISO 841 defines coordinate systems for machine tools: X, Y, and Z describe linear motion, while A, B, and C describe rotation around those axes. On a spinning lathe, the exact axis assignment depends on the machine design. Check the machine manual before mapping the chuck, forming roller, and tailstock. A mistaken sign or origin can send a roller away from the intended path.

Machine coordinates describe fixed positions relative to the machine; work coordinates describe positions relative to the part setup. Set the work origin deliberately, then verify it with a safe, slow dry run. Learn how the control handles jog, feed hold, single block, and emergency stop before running a program. The 2024 Deloitte and Manufacturing Institute study estimates that 3.8 million U.S. manufacturing jobs may be needed by 2033, with 1.9 million potentially unfilled. That skills gap makes clear, repeatable setup habits especially valuable.

Tips: Label each axis on a sketch, then jog one axis at a time and watch the actual motion. Keep the first test conservative. I still find axis labels confusing when machine layouts differ; pause and confirm rather than guessing.

Prepare the Workpiece, Tooling, and Spinning Parameters

Before programming a multi-axis CNC spinning lathe, check the blank against the part drawing. Confirm its material, thickness, diameter, and condition; a small edge nick can grow during forming. Deburr the rim, then clean the contact surfaces. Measure the blank again. Record the actual thickness, not just the nominal value.

Choose a forming roller with a smooth, undamaged profile that suits the part’s curves. Secure the blank evenly, and verify that it sits centered on the mandrel. Set tool offsets carefully, then check clearance across every programmed axis. A slow, dry run can reveal a collision or an awkward approach before metal is under pressure. Do not assume a correct-looking toolpath is safe.

Set spindle speed, feed, and pass depth to suit the material, thickness, roller geometry, and machine limits. Start conservatively on a test piece, and inspect for wrinkles, tearing, or uneven walls after each pass. Adjust one parameter at a time; changing several together makes the cause harder to identify. The first setup may still need refinement. Record the settings and measurements, including small deviations, so the next run starts with evidence rather than guesswork.

Create and Simulate a Basic Multi-Axis Spinning Program

A basic multi-axis spinning program starts with a clear part drawing and a defined blank. Mark the mandrel profile, finished diameter, material thickness, and safe tool approach points before entering coordinates. Choose axis movements that match the machine’s configuration. Keep the first job simple: one smooth contour, a short forming pass, and a retract path.

Build the path in small segments. Set spindle and feed values using the machine’s approved setup guidance. Add clearance moves so the roller avoids the mandrel, chuck, and blank edge. Then simulate the complete sequence with the stock, mandrel, and tool geometry loaded. Watch for collisions, sudden axis reversals, and unsupported material near the rim. A clean simulation helps, but it cannot confirm every real-world setup detail. Rough first drafts can be useful; they often reveal missing clearances.

Tips: Verify axis directions and compare the simulated profile with the drawing. Check the setup before running a guarded, low-speed trial, and follow the machine’s operating procedures.

How to Program a Multi Axis CNC Spinning Lathe for Beginners - Create and Simulate a Basic Multi-Axis Spinning Program

Example planning data for a simulated spinning pass on a 1.0 mm thick aluminum blank. Coordinates and settings are illustrative; verify them against the machine, tooling, material, and approved process before machining.

Step Operation X Position
(radius, mm)
Z Position
(mm)
C / Spindle
(rpm)
Feed
(mm/min)
Simulation Check
1 Load setup and define blank 60.0 0.0 0 — Confirm blank diameter, thickness, mandrel profile, and work offsets.
2 Safe approach to starting point 63.0 5.0 0 — Check clearance from the blank, roller, tailstock, and mandrel.
3 Start rotation and establish contact 60.0 5.0 400 40 Verify rotation direction and gradual roller engagement.
4 Rough forming pass toward mandrel 42.0 28.0 400 60 Inspect the toolpath for collisions and abrupt changes in direction.
5 Intermediate forming pass 30.0 38.0 500 50 Check material flow and the simulated part profile against the mandrel.
6 Finish pass along the profile 20.0 45.0 500 30 Review profile contact, feed continuity, and expected wall thinning.
7 Retract roller and stop rotation 63.0 5.0 0 — Confirm the roller clears the finished part before ending the cycle.
8 Review simulation and setup notes — — — — Check axis limits, clearance, spindle direction, and machine-specific coordinate conventions.

Coordinate note: X is shown as radius from the spindle centerline, Z is axial distance from the chosen front datum, and C / spindle is shown as rotational speed. Axis definitions and programming conventions vary by machine.

Run a Test Cycle, Inspect the Part, and Refine the Program

A multi-axis CNC spinning lathe can coordinate the spindle, forming rollers, and cross-slide, but a simulation cannot reveal every real-world issue. Before cutting, verify the stock size, tool clearance, workholding, and program coordinates against the setup sheet. Run the approved test cycle with guards closed, using the machine’s safe verification mode and reduced feed where appropriate. Watch for unexpected axis motion, vibration, or a roller approaching the blank too quickly. Stop if anything looks wrong. A cautious pause is cheaper than a damaged tool or part.

Inspect the first part against the drawing, not just by eye. Measure key diameters at several points, check the rim for waviness, and compare wall thickness where the material has stretched. A simple light reflection can reveal subtle ripples, but it cannot replace measurements. Let the part cool and settle before recording dimensions; heat can affect readings. Write down the actual values, tool position, and cycle settings. Small notes matter.

Refine one variable at a time, such as roller path, forming pressure, or feed rate, within approved process limits. Then run another controlled test and compare the results. If the part improves in one area but worsens elsewhere, keep that observation in the setup record. The first attempt may be uneven. That is useful feedback, not proof the whole program is wrong. Make changes deliberately, and have a qualified operator review the revised sequence before production.

How to Program a Multi-Axis CNC Spinning Lathe for Beginners

Run a test cycle, inspect the part, and refine the program.

Example inspection readings show diameter deviation from target at five axial stations. After refinement, all readings are within the example acceptance range of ±0.20 mm. Actual limits depend on the part drawing and process requirements.

FAQS

What does a multi-axis CNC spinning lathe do?

It presses a roller against a rotating metal blank over a mandrel. Controlled passes shape the metal.

What are the main machine components?

The spindle and chuck hold and rotate the blank. The mandrel supports its inner profile, while the roller forms the metal. Small details matter.

What do the machine axes control?

X often moves the roller across the workpiece, and Z moves it along its length. The C axis controls spindle position. Axis directions can vary, so check the machine manual.

What should I check before programming?

Confirm the blank’s material, thickness, diameter, and condition. Deburr its rim, clean the contact surfaces, and measure the actual thickness. A small nick can grow during forming.

How should I prepare the tooling and workpiece?

Choose a smooth roller suited to the part’s curves. Center the blank on the mandrel, secure it evenly, and check tool offsets and clearance.

How should I set spinning parameters?

Match speed, feed, and pass depth to the material, thickness, roller, and machine limits. Start conservatively on a test piece. The first pass may disappoint.

Why run a dry test cycle?

It can reveal collisions or awkward roller approaches before forming begins. Use the machine’s safe verification mode and reduced feed where appropriate. Stop if motion or vibration seems unexpected.

How should I inspect and refine the first part?

Compare it with the drawing. Measure diameters at several points, check rim waviness, and record wall thickness. Change one setting at a time, then compare another controlled test. A light reflection can reveal ripples, but measurements matter more.

Conclusion

This beginner-friendly guide explains how to program a multi axis cnc spinning lathe for beginners, starting with the machine’s purpose and main components. It introduces the axes, machine coordinates, and control functions so readers can understand how programmed movements shape a workpiece. The guide then covers practical preparation, including selecting and securing the workpiece, choosing suitable tooling, and setting initial spinning parameters.

Readers are guided through creating a basic multi-axis program and checking it in simulation before machining begins. The final steps focus on running a cautious test cycle, inspecting the finished part for accuracy and surface quality, and refining the program when adjustments are needed. By following this structured process, beginners can build confidence, improve consistency, and develop a safer, more methodical approach to CNC spinning.

Henry

Henry

Henry is a dedicated marketing professional with a profound expertise in the company's offerings. With years of experience in the industry, he possesses an impressive understanding of the market dynamics and consumer behaviors that drive success. Henry is committed to sharing his insights through......